High Performance: The repeat positioning accuracy of this CNC tool setter is up to 0.001mm, and the tool setting speed is 50 to 200mm per minute.
Good Stability: This tool setter has built in stroke , 4 layer sealed movement designed, completely resistant to oil and water, in use.
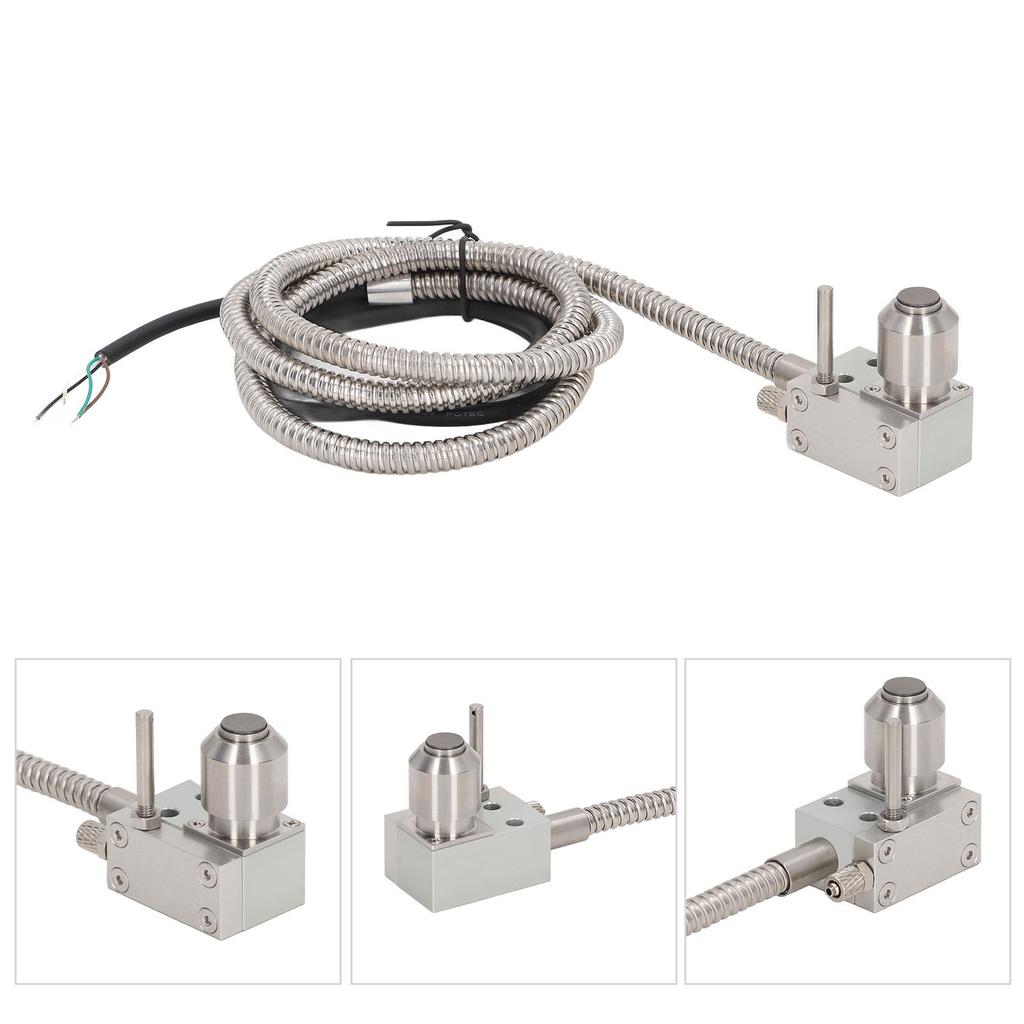
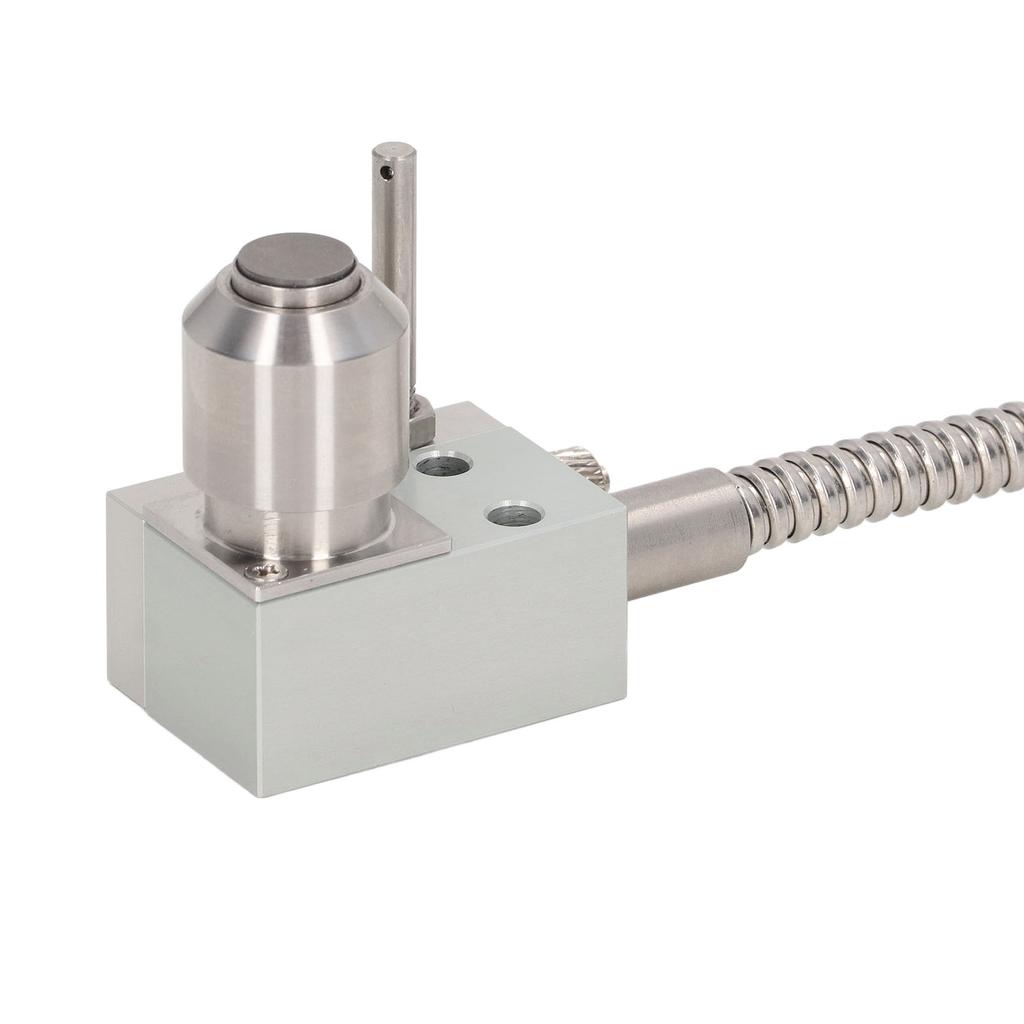
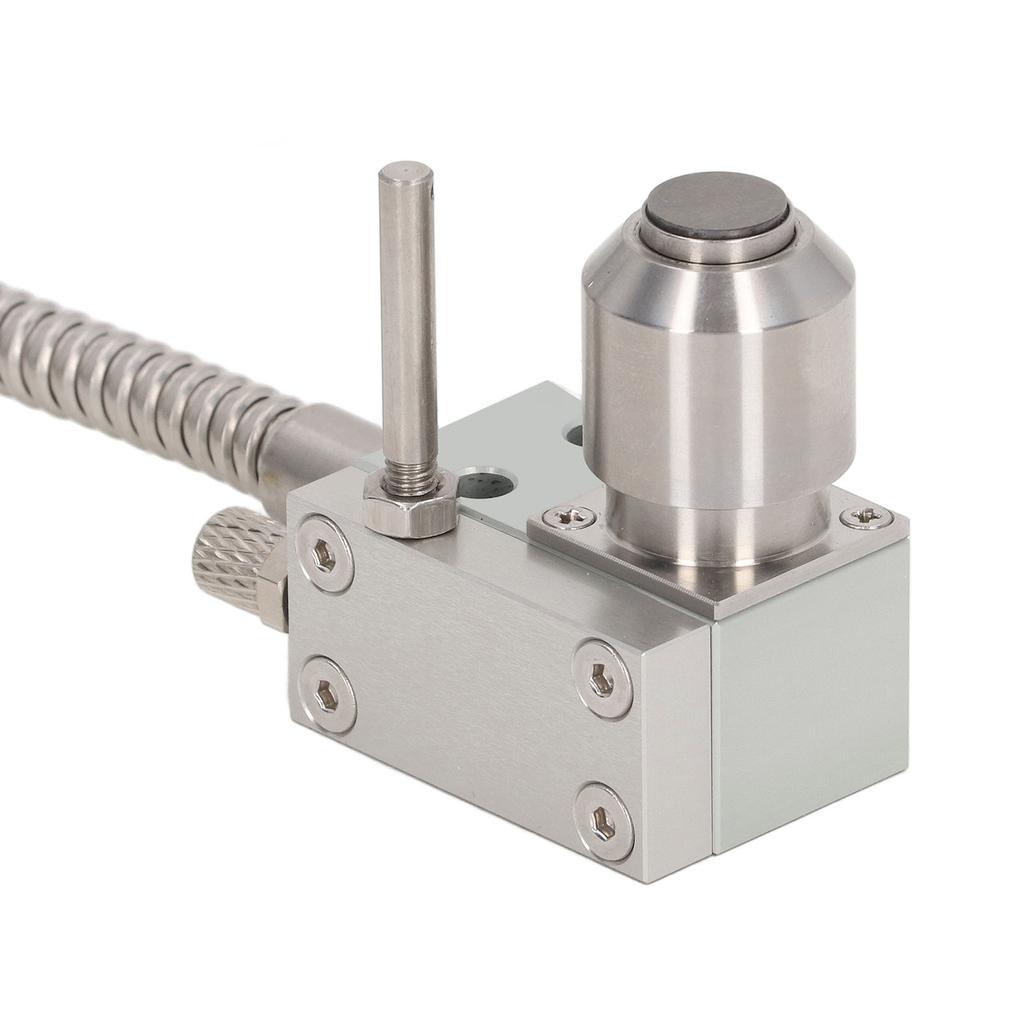
Umbrella Contact Head: One piece umbrella shaped contact head design can effectively prevent cutting powder and oil from splashing into the tool setter, ensuring high in harsh environments.
Item Type: Tool Setter
Material: Alloy steel
Tool Setting Speed: 50-200mm per minute
Contact Service Life: 3 million times
Positioning Accuracy: 0.001mm
Power Supply Voltage: 5-24V, current below 20mA (maximum), when with LED lamp, the current should be limited below 10mA
Ambient Temperature: 0 celsius to 80 celsius
: IP67 (100% waterproof, oil proof sealing)
Note:
Mechanical:
1. When the tool setting instrument is directly installed on the workbench with guaranteed spindle, right angle and parallelism, the installation shall be cleaned and fixed with .
2. When installing on other planes, find out the right angle and parallel of the mounting .
3. When using ive cover, pay special attention to the position of the used contact , right angle, repeatability of parallelism, temperature change of installation rod, and rigidity (related to the weight and contact force).
Electrical:
1. Contact rated +24V +Celsius- 10% 20mA (maximum)
2. When the machine body is grounded, the tool setting instrument should be installed at the side of the ground wire during connection.
3. When connecting the tool setting instrument with LED, pay attention to the polarity (+) (-). Recommended value: 10mA, resistance load.
There are three main forms of chip prevention:
1) Pipe
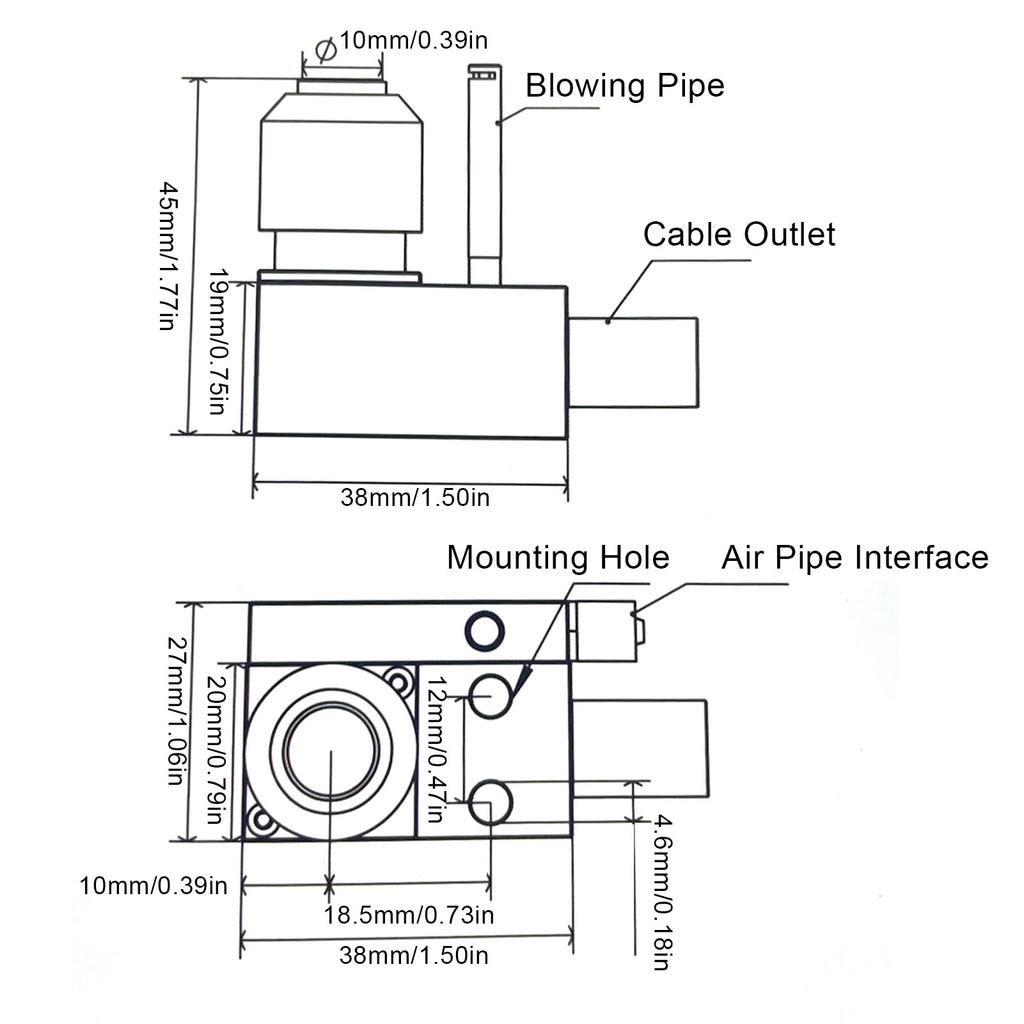
A. Blow off the chips and coolant attached to the contact s and tools. The grease and foreign matters that cannot be blown off and stick to the contact parts shall be cleaned frequently.
B. The screw joint at the tip of the pipe will be damaged when the tool and cutting chips are strongly impacted.
C. The inner Diameter of the pipe passage shall be set at more than 2.
2) ive Cover
A. In the environment with cutting chips, if a rubber cover is used to the cutting chips and coolant, which will hinder the of movable parts after accumulation, then a ive cover is required.
B. There are fixed (or detachable) and automatic types, can be used by the customer according to the situation.
3) Cleaning
A. The cutting chips and oil stains attached to the contact (super hard) that are difficult to blow off with should be cleaned with alcohol.
B. Around the rubber cover, the clearance between the rubber ive cover and the pipe, and the accumulation of cutting chips outside the ive cover may hinder the movement and return of the rubber. Please clean it.
C. Do not open the inside of the rubber ive cover.




 Возврат по недоставке


